An industrial high-frequency grinder is an electric grinding tool powered by a matched high-frequency converter or generator. For foundries and shipyards, selection starts with the job: casting fettling, flash removal, weld grinding, edge preparation or surface finishing. Match the tool size and abrasive to that task, then confirm the electrical supply and working duty.
This guide covers a practical workflow for selecting a foundry grinder or shipyard grinding system, including 180mm angle grinders, larger tools for heavier removal, straight grinders for restricted access, and compatible 250Hz or 300Hz power supplies.
Applications · Tool size · Abrasives · Power supply · Trial checklist
FUJI high-frequency grinders use a brushless, asynchronous squirrel-cage induction motor. The tool receives the specified electrical output from a suitable power source rather than being connected indiscriminately to ordinary mains power. The frequency in hertz is an electrical rating; it is not the spindle speed in RPM.
For repeated industrial metal removal, the useful question is how the complete system performs under the intended load. Check working speed, removal rate, tool temperature, abrasive wear and operator control together. High-frequency operation does not mean that speed never drops or that unlimited overload is permitted.
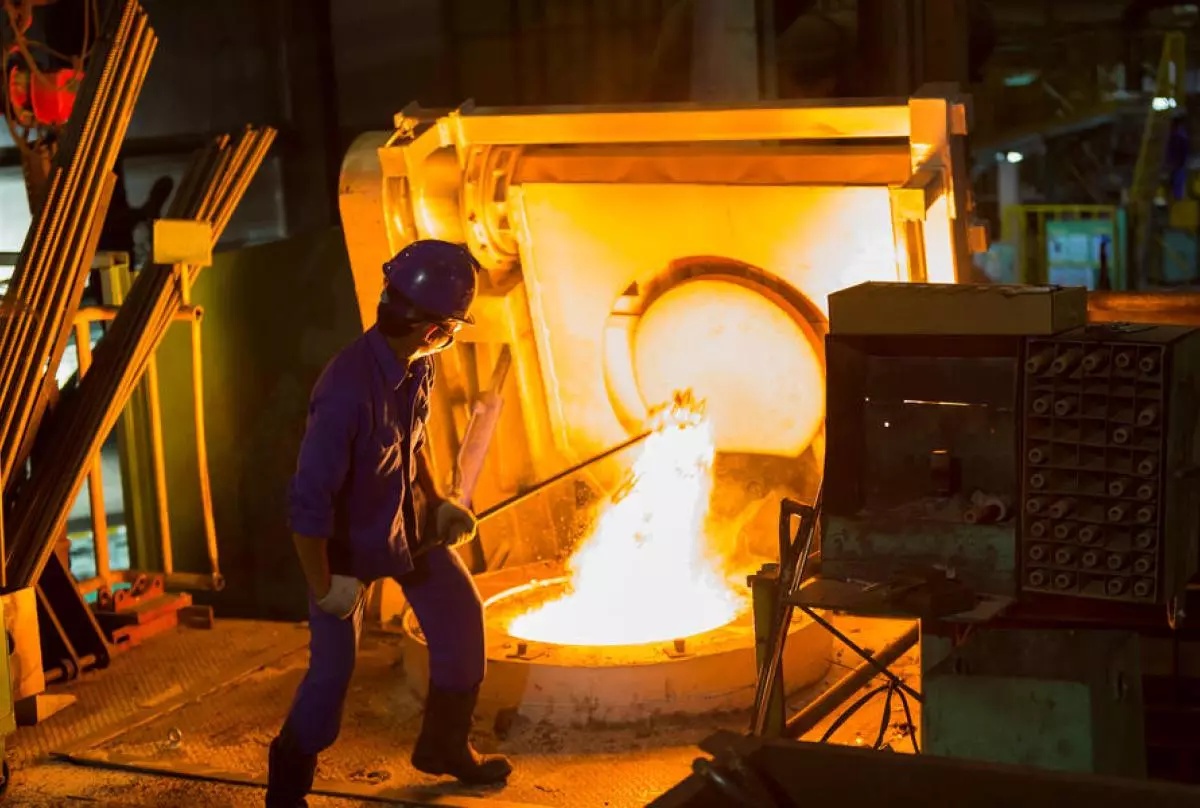
Fettling is the cleanup of a casting after production. On grey cast iron, ductile iron or cast steel, the task may involve removing flash, dressing parting lines or blending residual material after gates and risers have been removed. The alloy, remaining stock and required contour determine the appropriate abrasive and tool.
A broad casting face and a narrow flash line place different demands on the wheel. Record the contact area and amount of metal to remove rather than describing every job simply as heavy grinding. Where a large gate or riser must be cut off, assess a separate cutting operation with an approved cutting accessory and guard; a grinding wheel is not automatically a cutting wheel.
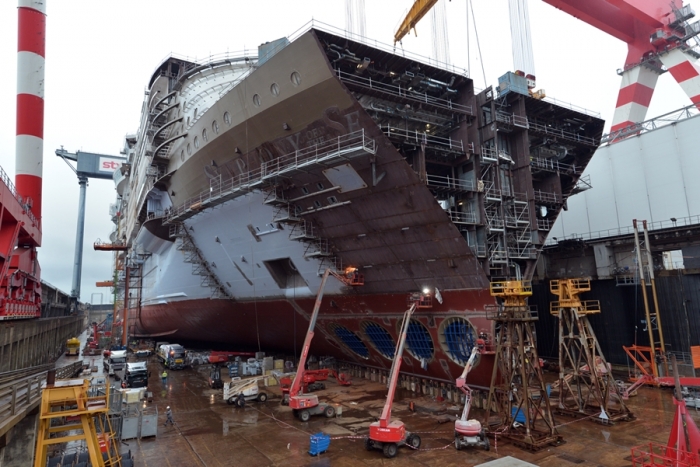
In shipbuilding and repair, a grinder may dress weld reinforcement, remove burrs from plate edges or blend a welded repair into the surrounding steel. Define the required profile first: excessive removal can damage the parent plate or reduce the intended weld section. Select the abrasive according to whether the job requires stock removal or finishing.
Large hull sections and changing work positions also make cable routing, access and power distribution part of the selection. Check whether the operator can control the tool at the required angle, and whether several stations will draw power at the same time. Rust or coating preparation should follow the specified surface-preparation method and contamination controls, rather than assuming a grinding wheel suits every coating-removal task.
| Task and access | Starting point | Selection check |
|---|---|---|
| Accessible casting faces, flash and steel welds | 180mm / 7-inch high-frequency angle grinder | Required removal, contact area, handling and permitted wheel |
| Large castings with substantial stock removal | Assess a 230mm / 9-inch high-frequency angle grinder | Model power, torque, weight, guard and available working space |
| Internal cavities or restricted casting features | High-frequency straight grinder with an approved mounted abrasive | Collet/shank fit, abrasive diameter, overhang and speed limit |
| Weld blending and surface finishing | Suitable angle grinder with a compatible flap disc | Grit, finish, edge control and disc speed rating |
The FUJI HGC-3902 180mm model has a rated power of 2600W and a tool weight below 5kg. Its size can balance access and material removal on suitable jobs, but the complete setup, working posture and duration still affect operator fatigue. A larger wheel is useful only when the machine, guard, task and workspace support it.
For internal features, review the FUJI high-frequency straight grinder range. Match the specific model and mounted accessory; a small abrasive diameter does not by itself establish a safe operating speed.
The grinder and consumable should be trialled as a pair. A powerful motor cannot compensate for the wrong abrasive formulation, excessive contact pressure or a wheel that does not suit the material.
Confirm diameter, thickness, bore, permitted operation and marked maximum RPM against the exact grinder specification. Keep material-specific abrasives separate where the job requires contamination control.
Check the output nameplate on the converter or generator. Its output frequency, voltage, phase configuration and capacity determine which grinders can be connected. The incoming factory mains supply and the high-frequency output are different specifications: tool selection must follow the output supplied to the grinder.
Frequency identifies the required electrical configuration. It does not, by itself, establish which tool has a longer service life, lower vibration or better grinding performance. Compare the actual machine, abrasive and working conditions.
The FUJI HGC-3902 300Hz angle grinder provides a heavy-duty option for facilities using matching European high-frequency power supplies. It can support tool replacement or additional grinding stations while retaining suitable existing infrastructure.
A FUJI 250Hz grinder and power-source combination suits facilities using Japanese-standard high-frequency equipment, or new stations configured around a matching 250Hz supply.
| Facility configuration | Suitable starting point | Confirm before ordering |
|---|---|---|
| Existing three-phase 200V, 300Hz supply | Matching FUJI 300Hz angle or straight grinder for the task | Tool ratings, connector arrangement, power-source condition and capacity |
| Existing 250Hz supply | Matching FUJI 250Hz angle or straight grinder for the task | Output voltage, tool ratings, connections and capacity |
| New station without a high-frequency supply | A complete 250Hz or 300Hz tool and power-source combination | Available input power, number of operators, cable layout and service requirements |
| Workshop operating both systems | Dedicated tools matched to each supply | Clear identification of tools, outlets and cables to prevent incorrect connections |
Replacing a worn grinder does not automatically require changing the facility's frequency standard. Retain an appropriate working power system when it meets the new tool's requirements. If a power source needs replacement, select its replacement around the planned tool fleet and production needs.

For a focused replacement checklist, see our 300Hz foundry grinder replacement guide.
Compare tools on the same material and a repeatable task. A short demonstration on an easy edge is not evidence for an entire production shift. Include the intended contact area, working posture and normal pause pattern.
| Record | Why it matters |
|---|---|
| Workpiece grade, starting condition and target profile | Makes removal and finish results comparable |
| Time per part and metal removed | Shows useful output; mass removed divided by time gives mass removal rate |
| Wheel specification and mass loss | Reveals abrasive consumption alongside output |
| Power-source ratings and simultaneous users | Identifies the actual system conditions during the trial |
| Working speed, temperature and stops | Helps assess load response and duty suitability |
| Finish, handling and exposure assessment | Checks whether faster removal also meets quality and workplace requirements |
For a purchasing comparison, include abrasive cost, productive time, disc changes and rework per accepted part. Do not assume every HF tool has lower vibration than every pneumatic or conventional electric grinder. Assess the actual tool, accessory and exposure duration. The HSE foundry fettling case study illustrates why vibration exposure still needs control when high-frequency grinders are used.
Use a representative trial to compare job time, wheel consumption, handling and finish. Record the tool, supply, abrasive and workpiece used so that the results can guide repeat purchasing.
Consider it for repeated fettling and metal-removal tasks where a compatible supply can serve the work area. Compare a complete tool, power-source and abrasive combination against the current process using representative castings, rather than selecting by frequency alone.
No. It is a useful starting point for accessible surfaces and edges. Large removal volumes may justify assessing a larger tool, while internal features can require a straight grinder. Access, weight, required contour and approved abrasive size determine the choice.
Potentially, when its output voltage, frequency, phase, capacity and protective arrangements match the selected tool. Connector fit alone is not sufficient. Send the converter and grinder nameplates for confirmation before connection.
Do not assume interchangeability. Use the ratings specified for the exact model; multi-frequency operation requires explicit manufacturer support. Both systems can serve demanding grinding tasks when correctly configured.
For suitable steel work, Super F2 is an economical grinding option; Super Z is a candidate for heavier removal. A suitable flap disc can blend and refine the surface. Select the exact grade and size by material, required finish and tool rating.
No. Load response and permitted duty depend on the motor, supply, abrasive and operating conditions. Follow the model instructions and validate the intended work cycle; frequency alone does not establish an unlimited-duty rating.
Send your power-source nameplate and grinding requirements to FUJI. Our team can help match a 300Hz or 250Hz grinder, power supply and abrasive to your foundry or shipyard application.
Discuss Your Grinding Configuration


